PRODUCTS FOR FOUNDRIES
Refractory coatings are applied to sand moulds and cores in foundries (steel castings, grey cast iron and ductile iron, and non-ferrous metals).
Refractory coatings provide a protective barrier between the molten metal and the mould or core substrate during the casting process, ensuring the integrity of the cast surface and preventing defects, such as segregations, burnt-in sand, bulges/recesses and other.
They reduce the thermal shock caused by sand substrate and reactions between the substrate and melt, strengthen the mould surface and give smooth surface of castings.
Different applying processes can be used for our coatings – dipping, spraying, pouring and applying with brush – providing flexible use in production processes specific to individual foundries. Efficient coating must provide the following features:
- Sufficient refractory quality to prevent melt being pured into substrate
- Good adhesiveness to substrate and good covering characteristics
- No blistering, cracking and scaling tendency on drying
- Good suspension and mixing properties
- Good storage stability
- Good adhesiveness
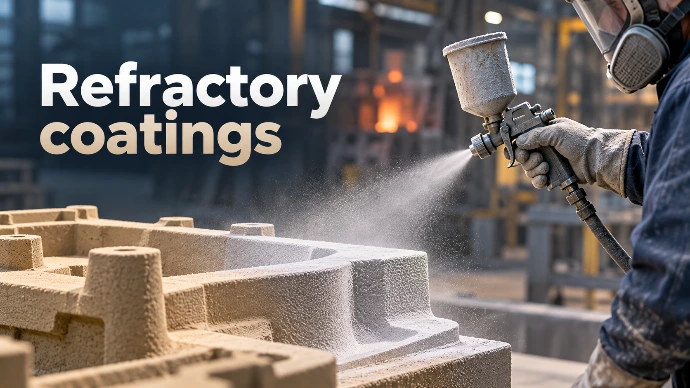
Refractory coatings
Water-based and alcohol-based coatings for sand moulds and cores.
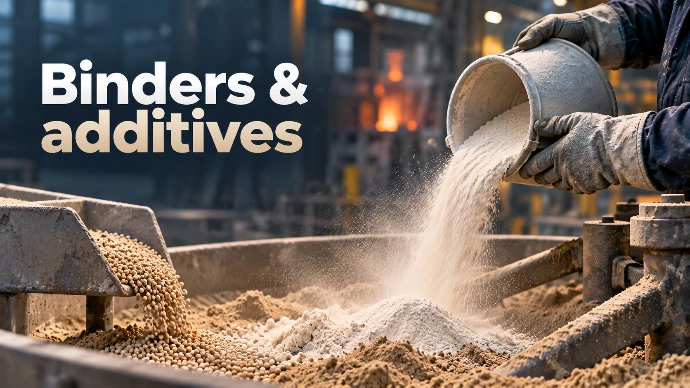
Binders & additives
Silicate binders and additives for CO₂-cured sand moulds and cores.
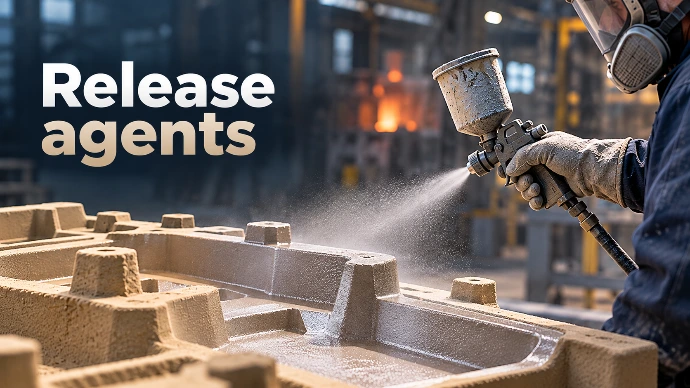
Release agents
Materials supporting the separation of moulds and cores from patterns and core boxes.
Refractory Coatings for Sand Moulds and Cores
Refractory coatings form a protective interface between molten metal and the sand mould or core. When correctly selected and applied, they help control metal penetration, sand burn-on, metal–sand reactions and surface irregularities. The result is improved casting surface quality and more consistent finishing conditions.
EXOTERM coatings can be applied by brushing, dipping, spraying or flow coating, depending on product grade and process. Selection should consider the alloy, pouring conditions, sand system, target coating layer and drying method.
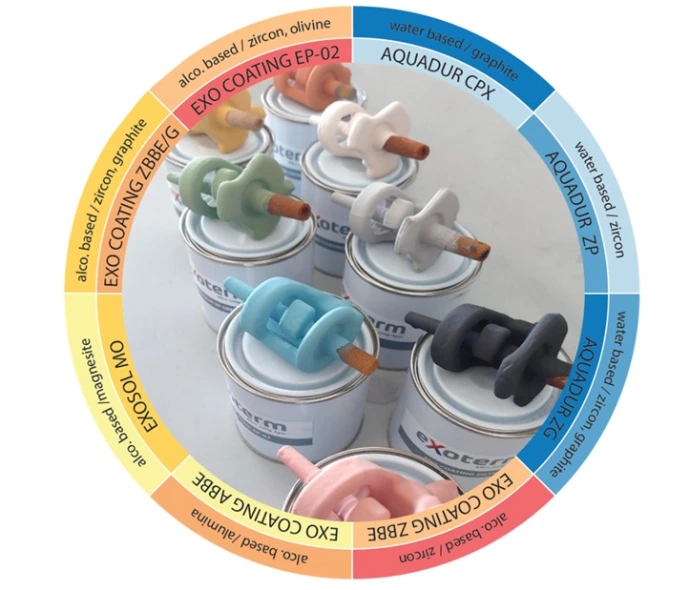
Water-based refractory coatings — AQUADUR
Water-based coatings are suitable for foundries looking for application flexibility without alcohol-based carriers. The formulation and dilution requirements depend on the specific product grade.
| Grade | Basic composition | Typical applications* | Key characteristics | Application guidance from supplied product summary |
|---|---|---|---|---|
| AQUADUR CPX | Graphite | Aluminium and copper alloys; grey and ductile cast iron | High refractoriness and favourable physicochemical properties | Brush: 5–10 wt.% water; dip/spray/flow: 10–20 wt.% water |
| AQUADUR ZP | Zircon | Grey and ductile cast iron; steel castings | High solids content and high refractoriness | Brush: 5–10 wt.% water; dip/spray/flow: 10–20 wt.% water |
| AQUADUR ZG | Zircon, graphite | Grey and ductile cast iron | High solids content and high refractoriness | Dip/spray/flow: approximately 35 wt.% water |
| AQUADUR K 22 | Silicate | Grey and ductile cast iron | Good physicochemical properties and refractoriness | Brush: 5–10 wt.% water; dip/spray/flow: 10–20 wt.% water |
Alcohol-based refractory coatings — EXO COATING
Alcohol-based grades offer an alternative drying and application route. Suitable dilution, drying, ventilation and safe handling must be assessed for the actual production conditions.
| Grade | Basic composition | Typical applications* | Key characteristics |
|---|---|---|---|
| EXO COATING BBE | Graphite, silicate | Aluminium and copper alloys; grey and ductile cast iron | High refractoriness and good physicochemical properties |
| EXO COATING ZBBE | Zircon | Grey and ductile cast iron; steel castings | High solids content and refractoriness |
| EXO COATING ZBBE G | Zircon, graphite, silicate | Aluminium and copper alloys; grey and ductile cast iron | High solids content and refractoriness |
| EXO COATING ABBE | Aluminium oxide | Grey and ductile cast iron; steel castings | High refractoriness and good physicochemical properties |
| EXO COATING EP 02 | Olivine, zircon | Grey and ductile cast iron | Special refractory coating with versatile application potential |
| EXO COATING L 25 ORANGE | Aluminosilicate | Aluminium and copper alloys; grey and ductile cast iron | High solids content and refractoriness |
| EXO COATING MO | Magnesite | Steel castings and manganese steel | High solids content and refractoriness |
Application: For brushing, the listed alcohol-based coatings are generally used at supplied viscosity. For dipping, spraying or flow coating, adjust with compatible EXO COATING RAZREDČILO (diluent) according to the grade-specific technical instructions. EXO COATING EP 02 is listed for brushing, dipping or spraying.
Technical note: *Application ranges and dilution values above are taken from the supplied product tables, not universal process guarantees. Verify current grade designation, technical data sheet and trial conditions before production use.
How to Select the Right Foundry Coating
Casting alloy
Specify aluminium, copper alloy, grey cast iron, ductile cast iron, steel or manganese steel. The alloy narrows the suitable refractory filler and grade.
Mould and core system
Identify the sand type and binding process, including CO₂, cold-box, hot-box, shell moulding or other relevant systems.
Application process
Specify brushing, dipping, spraying or flow coating, along with practical layer thickness and drying constraints.
Defect or production target
Explain the problem to solve: burn-on, penetration, surface roughness, coating cracks, drying time or consumption.
Silicate Binders and Additives for Sand Moulds and Cores
EXOTERM supplies silicate binder systems based on water glass for producing sand moulds and cores, including CO₂-hardening applications. Product selection depends on the sand, casting conditions and required shakeout behaviour.
VEZIVO MX — R, 7, 11, 15
Silicate binderBreakdown additive
A family of silicate binders incorporating an additive intended to improve breakdown of moulds and cores after casting. The supplied summary highlights consistent binder quality.
VEZIVO M
Silicate binder
Silicate binder for sand moulds and cores without an integrated breakdown additive. The supplied summary highlights consistent binder quality.
BETASIL 10
Liquid additiveFor VEZIVO M
A liquid additive intended to improve breakdown after casting. The supplied technical summary also identifies reduced storage sensitivity of CO₂-cured moulds and cores and potential reduction in binder consumption.
Release Agents for Patterns, Core Boxes and Moulding Tools
Release agents help reduce sticking of sand mixtures to patterns and core boxes, supporting cleaner release and repeatable mould and core manufacture. Choose the release agent for the tooling material, binder system and operating conditions.
LOČILEC GS/C
Silicone emulsionCroning / shell moulding
Forms a thin release film to reduce the adhesion of Croning sand to patterns and core boxes during binder curing.
ALUTIL AM-100
Aluminium paste & additives
Release agent for CO₂-bonded, furan-bonded and fresh bentonite sand mixtures. According to the supplied summary, it can be used on metal, plastic and wooden patterns.
Additional products in the existing range: TEXOL A for bentonite moulding; ALUTIL AMF, ALUTIL MOP 417 and ALUTIL MOP 461 for applicable metal mould and die-casting operations. Contact EXOTERM for the grade-specific selection and current technical documentation.
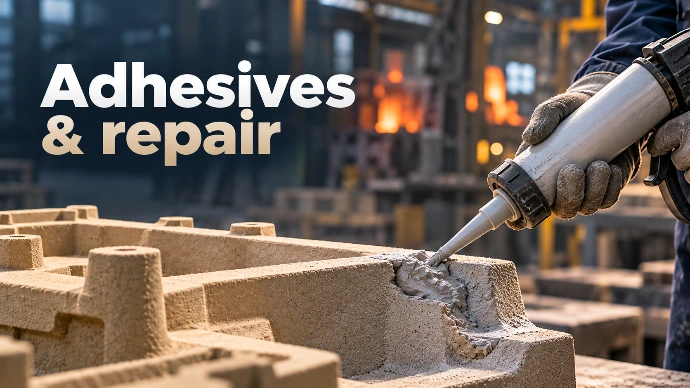
Adhesives and Mould Repair Materials
POPEX
Adhesive for joining sand moulds and cores, with applications across CO₂, Croning, cold-box, hot-box and bentonite moulding processes subject to grade suitability and production trials.
KITEX-C
Repair material intended for correcting local defects or damage in sand moulds and cores before casting, according to the applicable process instructions.
Foundry Process Optimisation and Technical Support
Product performance depends on the full casting process, not only the consumable. EXOTERM can work with customers to assess coating selection, application consistency, product consumption and casting quality. Technical support may include laboratory evaluation, comparative product trials and formulation adaptation to process-specific requirements.
Learn more about EXOTERM Research & Development services.
Frequently asked questions
Consider the drying method and available drying time, ventilation and handling requirements, mould or core system, application method and casting alloy. Confirm the choice through trials with a suitable grade.
The supplied selection table lists AQUADUR ZP, EXO COATING ZBBE, EXO COATING ABBE and EXO COATING MO among the steel-casting options. EXO COATING MO is also listed for manganese steel. Final selection requires the process conditions.
Many grades support spraying and dipping, but recommended dilution depends on the coating. Always follow the specific technical data sheet and validate the application procedure.
Share your alloy, moulding/core-making process, sand type, casting size, application method, current consumption, drying conditions and any relevant casting defects.
Find the Right Solution for Your Foundry
Tell us about your alloy, moulding technology, production conditions and casting quality targets. Our team can help you identify suitable products and plan practical trials.